PP & Packaging Material Ink Series

H633P

H633P PP No-Treatment Chemical Resistant Ink

A single-component, low-odor solvent-based ink developed for direct printing on selected untreated PP substrates without surface treatment.

No Surface Treatment RequiredStrong AdhesionAlcohol & Chemical ResistanceAbrasion Resistance
Printing Method
Screen Printing & Pad Printing
Recommended Substrates
Untreated PP Containers · PP Caps · PP Sheets · PP Housings · Other PP Components
Printing MethodScreen Printing & Pad Printing
Ink TypeLow-odor solvent-based PP ink
Component TypeSingle-component
Surface TreatmentNot required for selected untreated PP substrates
Recommended SubstratesSelected untreated PP components
Main ApplicationDirect printing on selected untreated PP

PRODUCT SUMMARY

H633P at a Glance

Primary Substrate Focus
Suitable or selected untreated polypropylene
Printing Methods
Screen printing and pad printing
Direct-Printing Scope
Evaluation without mandatory pretreatment for suitable PP materials
Verification
Adhesion and resistance testing on the actual finished part is recommended

KEY PERFORMANCE

Performance built around the printed finish

01

No Surface Treatment Required

Direct printing on selected untreated PP substrates.

02

Strong Adhesion

Excellent adhesion on selected untreated PP plastic parts.

03

Alcohol & Chemical Resistance

Excellent alcohol and chemical resistance under the stated conditions.

04

Abrasion Resistance

Good abrasion resistance for durable PP decoration.

RECOMMENDED SUBSTRATES

Confirmed compatible materials

Performance depends on substrate, surface treatment, printing process and drying or curing conditions. Substrate testing is required before production.

Untreated PP ContainersPP CapsPP SheetsPP HousingsOther PP Components

DIRECT PRINTING

Printing Directly on Untreated Polypropylene

Can polypropylene be printed without flame or corona treatment?
Some suitable untreated PP materials can be evaluated for direct printing, but polypropylene is a broad material category and adhesion depends strongly on the actual grade, finished part, surface condition, printing process, drying and required test standard.
Do I always need a PP primer before printing?
A primer is not mandatory for every suitable untreated PP application, but it may still need evaluation when the actual material is difficult to bond or the required adhesion and resistance cannot be achieved through direct printing.
What ink can print directly on untreated PP?
Evaluate an ink system specifically documented for selected untreated polypropylene, then verify adhesion and resistance on the actual molded or finished part. Hongsheng H633P is one system developed for this direct-printing evaluation.
Can untreated PP be screen printed or pad printed?
H633P supports both screen printing and pad printing on selected compatible untreated PP substrates. Confirm the exact material, process setup, drying condition and required performance before production.

ADHESION DIAGNOSIS

Common Adhesion Problems on Untreated PP

Why does ink peel off untreated polypropylene?
Peeling can relate to the exact PP grade, ink and substrate compatibility, surface condition, contamination, drying condition, printing conditions or the required adhesion standard. Check each factor on the actual part rather than assuming one universal cause.
Why can the same ink adhere to one PP part but fail on another?
PP covers many grades and finished parts. Differences in grade, additives, molding conditions and the actual part can change printing performance, so approval should be based on representative production samples.
Why can a PP print look good but fail a 3M tape or cross-cut adhesion test?
Visual appearance alone does not confirm adhesion. Confirm actual-substrate compatibility, complete drying and the customer's required tape or cross-cut method before accepting the result.
Why can adhesion change during production?
Review material batches, surface condition, contamination, ink-film consistency, printing setup, drying temperature, drying time and ventilation. Recheck adhesion whenever a production variable changes.

TREATMENT DECISION

Printing Untreated PP: When Is Surface Treatment Still Necessary?

Does untreated-PP ink mean flame or corona treatment is never required?
No. H633P should not be interpreted as a universal no-treatment-required ink for every PP grade. Direct printing must be confirmed on the actual material against the required test standard.
Can every PP grade be printed directly?
No. The actual PP grade and finished part can behave differently, even when both are identified as polypropylene. Use representative parts for printing, drying, adhesion and resistance trials.
When should pretreatment or primer still be considered?
Evaluate treatment when the PP grade is difficult to bond, the required adhesion standard is unusually demanding, production conditions differ from the tested setup, or direct-printing trials do not meet the required result.
What if pretreatment is already part of the production process?
Hongsheng should review the existing treatment system, printing method and performance requirement before selecting the appropriate PP ink system rather than forcing H633P into the process.

PERFORMANCE VERIFICATION

Meeting Adhesion & Resistance Requirements

What should be checked if untreated PP fails a 3M tape test?
Confirm the actual PP grade, surface cleanliness, ink compatibility, printing conditions and complete drying, then repeat the specified tape or cross-cut test on a representative part.
How should cross-cut adhesion be evaluated?
Use the documented 1 mm × 1 mm, 100-grid cross-cut and 3M tape peel as the H633P reference where applicable, while also confirming the customer's required method and acceptance standard.
What should be checked when alcohol or gasoline resistance is required?
Confirm the required liquid, load, number of double rubs, drying condition, acceptance criteria and actual end use. Compare those requirements with the documented H633P reference conditions below.
What tests should be confirmed before mass production?
Confirm the required adhesion, alcohol, abrasion, gasoline, chemical or immersion tests, then run them on representative production parts after complete drying.
RequirementDocumented H633P Reference
Adhesion100/100 squares retained · 1 mm × 1 mm, 100-grid cross-cut; 3M tape peel
Alcohol resistanceNo visible change · 500 g load; 100 double rubs
Abrasion resistanceNo substrate exposure · 500 g load; 500 double rubs
Gasoline resistanceNo visible change · 500 g load; 50 double rubs
Acid resistanceNo visible change · 5% HCl immersion for 24 h
Alkali resistanceNo visible change · 5% NaOH immersion for 24 h
Salt-water resistanceNo visible change · 5% NaCl immersion for 24 h
Water resistanceNo visible change · Tap-water immersion at 20°C for 96 h

Reference data reflects documented H633P test conditions. Actual results may vary with the PP grade, finished part, ink color, film thickness, drying conditions and production process.

PRODUCT SELECTION

How to Choose Ink for Untreated PP Screen & Pad Printing

What should buyers compare when choosing ink for untreated polypropylene?
Compare exact PP compatibility, treatment requirement, screen or pad printing, adhesion and resistance requirements, drying and production needs, consistency, actual-part testing and available technical support.
What should be considered when choosing between direct printing and surface treatment?
Evaluate the actual PP grade, required adhesion and resistance, production process, equipment, added treatment steps and production stability. Do not assume that skipping treatment is appropriate until the direct-printing result is verified.
Is untreated-PP ink more cost-effective than using pretreatment?
Total process cost can include ink, treatment equipment, primer, labor, production speed, rejection rate, adhesion consistency, resistance performance and technical support. Hongsheng can evaluate the actual PP application before recommending a system.

DIAGNOSTIC PATH

Untreated PP Printing Troubleshooting

  1. 1
    Confirm the material

    Verify that the part is actually polypropylene rather than another low-surface-energy plastic.

  2. 2
    Identify the PP grade and part

    Record the resin grade where known and use the actual molded or finished part for testing.

  3. 3
    Confirm treatment status

    Check whether flame, corona, plasma, primer, coating or another treatment has already been used.

  4. 4
    Check surface condition

    Remove dust, oil, mold-release residue and other contaminants before printing.

  5. 5
    Confirm the printing setup

    Verify whether screen or pad printing is used and keep the production setup consistent.

  6. 6
    Confirm drying conditions

    Use the documented H633P guidance: hot air at 40–60°C, recommended 50°C; full drying by 24-hour air dry or 80°C oven cure for 30 minutes.

  7. 7
    Evaluate adhesion

    Test after complete drying using the customer's required adhesion method.

  8. 8
    Verify required resistance

    Run the required alcohol, gasoline, chemical or other resistance tests where relevant.

  9. 9
    Select the appropriate Hongsheng system

    Use H633P only where the confirmed material, process and performance scope matches; otherwise evaluate treatment or another suitable ink system.

APPLICATION BOUNDARIES

When H633P May Not Be the Right Ink

H633P is not guaranteed for every polypropylene grade, and not every untreated low-surface-energy plastic is PP. It should not automatically be recommended for PE, HDPE or unrelated plastics outside its confirmed scope.

Unusually demanding adhesion or chemical-resistance requirements require actual-part testing. If pretreatment or PP primer is already part of the process, or direct-printing trials do not meet the required result, Hongsheng should evaluate another suitable PP ink system.

TECHNICAL INFORMATION

Technical Information

Key reference data for product selection and printing evaluation.

Product Type
Single-component, low-odor solvent-based ink
Printing Method
Screen Printing & Pad Printing
Recommended Substrates
Selected untreated PP containers, PP caps, PP sheets, PP housings and other PP components
Component Type
Single-component
Surface Treatment
No surface treatment required for selected untreated PP; difficult substrates may require PP-P1 after testing
Surface Drying
Hot air: 40-60°C (Recommended: 50°C)
Full Drying
Air dry for 24 hours, or oven cure at 80°C for 30 minutes
Screen Mesh
100-130T
Dry-Film Gloss
≥ 65 GU - 60° gloss meter
Adhesion
100/100 squares retained - 1 mm × 1 mm, 100-grid cross-cut; 3M tape peel
Alcohol Resistance
No visible change - 500 g load; 100 double rubs
Abrasion Resistance
No substrate exposure - 500 g load; 500 double rubs
View Additional Test Data
Ink Fineness
≤ 12 μm - grind gauge
Acid Resistance
No visible change - 5% HCl immersion for 24 h
Alkali Resistance
No visible change - 5% NaOH immersion for 24 h
Salt-Water Resistance
No visible change - 5% NaCl immersion for 24 h
Water Resistance
No visible change - tap-water immersion at 20°C for 96 h
Gasoline Resistance
No visible change - 500 g load; 50 double rubs

Test results are for reference only. Actual performance depends on substrate, surface treatment, printing process and drying conditions.

Technical notes
  • Remove dust, oil, mold-release residue and other contaminants before printing.
  • Conduct a production trial before mass printing.
  • Drying and performance vary with substrate, surface treatment, film thickness, temperature and ventilation.
  • Shelf life: 12 months from manufacture in unopened original packaging; re-test expired material.

STANDARD COLORS & SPECIAL EFFECTS

Catalog Color Range

Standard, metallic, fluorescent and transparent colors shown in the catalog are available as reference options. Final appearance must be confirmed on the actual substrate.

PACKAGING OPTIONS
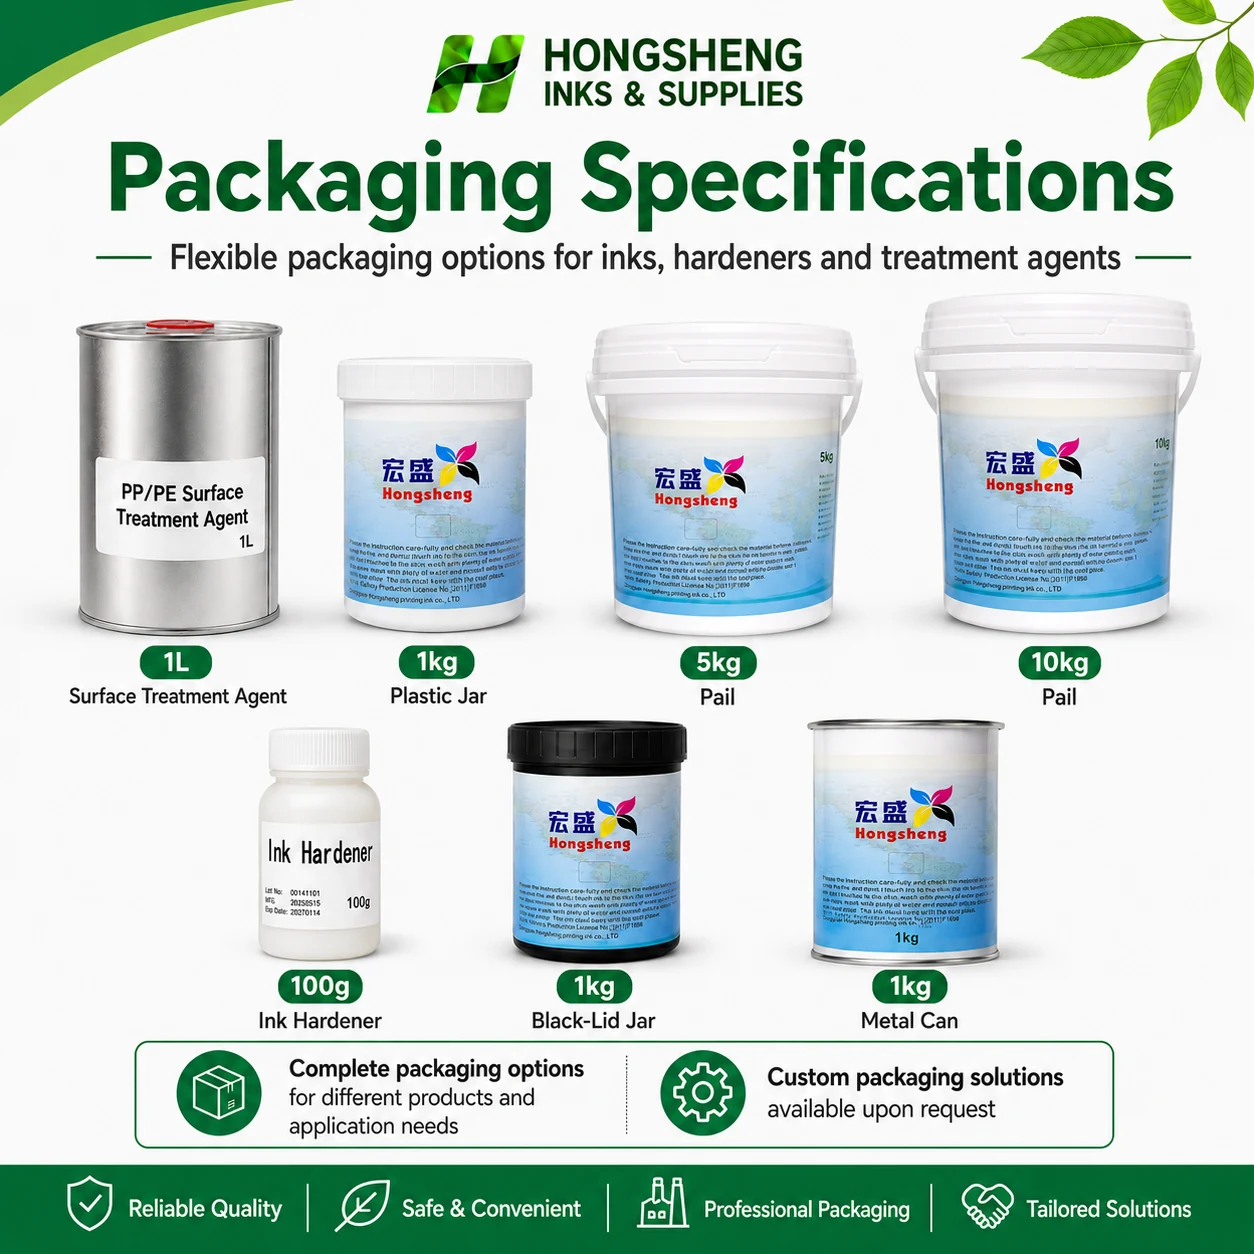
Packaging options

1 kgPlastic jarStandard package
5 kgPailGeneral packaging option
10 kgPailGeneral packaging option
CustomCustom packagingAvailability upon request
Hongsheng general packaging specifications
Hongsheng product compliance documentation scope

COMPLIANCE & DOCUMENTATION

Product documentation scope

The available documentation scope for this product includes the items shown below. Please identify the required color and destination market when requesting the applicable report.

  • Product- and color-specific compliance documentation is available upon request.
  • Confirm the destination market and required test scope before ordering.
Request Compliance Documents

APPLICATION EVALUATION

Information Helpful for Application Evaluation

Provide the available details below so Hongsheng can diagnose the material, treatment status, printing process and required tests before recommending H633P or another suitable PP ink system.

  • Exact substrate
  • Confirmation that the material is PP or polypropylene
  • Resin grade, if known
  • Actual molded sample or finished part
  • Untreated, flame-treated, corona-treated or primer-treated status
  • Screen printing or pad printing
  • Ink color
  • Current printing problem
  • Drying conditions
  • Current ink system, if relevant
  • Required adhesion standard
  • 3M tape test requirement
  • Cross-cut requirement
  • Alcohol resistance requirement
  • Gasoline or chemical resistance requirement
  • End-use environment

TECHNICAL & CUSTOMIZATION SUPPORT

Support around the substrate, color and printing process

Custom Color Matching

Match the required appearance using the confirmed substrate and reference.

Formula Adjustment

Review adhesion, drying and resistance requirements together.

Compatibility Testing

Evaluate the actual substrate, treatment and printing conditions.

Printing Troubleshooting

Review leveling, edge definition, adhesion and drying issues.

Discuss Your Application

WHY CHOOSE HONGSHENG

Focused support for industrial printing projects

Customized formulationSubstrate testing supportFlexible packaging supportConsistent product performance
Learn More About Hongsheng →